The global industrial landscape relies heavily on the seamless transfer of power and synchronization, where high-quality rubber components play a pivotal role. In the realm of automotive and industrial machinery, the procurement of reliable parts through wholesale conveyor belt channels ensures that businesses can maintain operational efficiency while reducing downtime. Understanding the technical nuances of these components is essential for any procurement manager seeking to balance cost and performance.
From the intricate timing systems of a modern combustion engine to large-scale industrial transport, the demand for precision-engineered rubber belts is ever-growing. The ability to source these components in bulk allows manufacturers to standardize their maintenance cycles and ensure that critical systems, such as engine valves and pistons, remain perfectly synchronized. This systemic reliability is what separates high-performance machinery from those prone to catastrophic failure.
When exploring options for wholesale conveyor belt and timing solutions, it is crucial to recognize that a belt is more than just a strip of rubber; it is a critical "bridge" for force transfer. By focusing on material durability and precise tooth geometry, industries can prevent the devastating internal engine damage that occurs when a timing belt fails.
The Role of Timing Systems in Automotive Engineering
In the complex working process of an automobile engine, four critical stages—air intake, compression, explosion, and exhaust—occur continuously within the cylinder. To ensure the engine operates without internal collision, the timing of each step must match the motion state and position of the piston exactly. The timing belt serves as the essential "bridge" in this process, transferring the rotational force from the crankshaft to the corresponding camshafts and valves.
Because the precision of this synchronization is so vital, any failure in the belt can lead to catastrophic damage to the internal valves. This is why many high-end vehicles utilize metal chains for ultimate stability, yet rubber belts remain a preferred choice for many due to their noise reduction and efficiency. For those managing fleets, sourcing through wholesale conveyor belt and timing belt suppliers ensures a steady stream of replacement parts to maintain these strict timing requirements.
Defining Precision in Rubber Belt Procurement
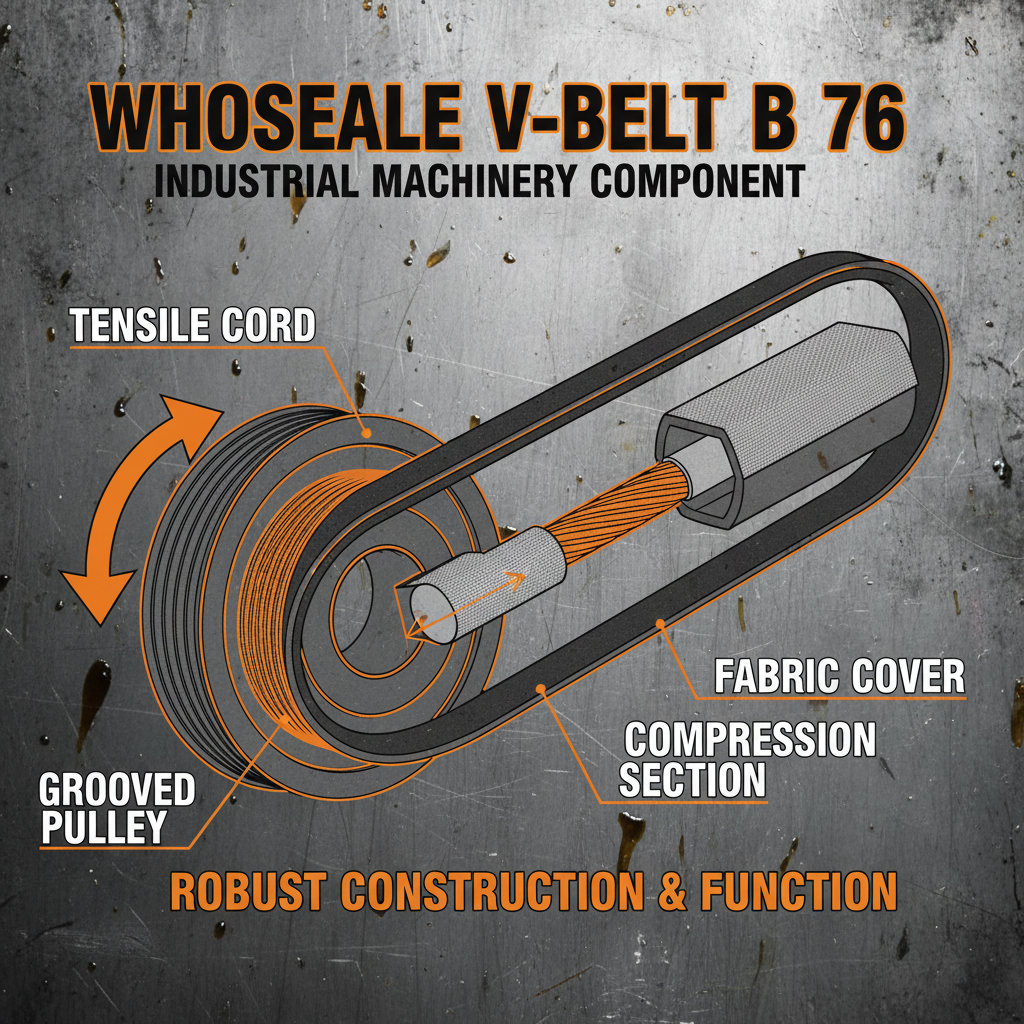
At its core, the concept of procuring a wholesale conveyor belt or timing belt refers to the bulk acquisition of synchronized power transmission components designed to meet specific industrial or automotive tolerances. Unlike standard flat belts, these precision components feature teeth or ribs that prevent slippage, ensuring that the driving and driven components remain in a fixed positional relationship.
In modern industry, this precision is not merely a luxury but a necessity for humanitarian and commercial infrastructure. Whether it is a timing belt in a medical device or a heavy-duty belt in a food processing plant, the ability to maintain exact timing prevents mechanical failure and ensures worker safety. The integration of advanced rubber compounds allows these belts to withstand varying temperatures and chemical exposures.
By streamlining the supply chain through wholesale channels, companies can ensure that they have the exact specifications required for their specific machinery. This removes the risk of using "near-fit" components, which often lead to premature wear or catastrophic synchronization failure in high-stress environments.
Core Factors Affecting Belt Durability
One of the primary factors in the longevity of a wholesale conveyor belt or timing system is the quality of the rubber compound used. Over time, rubber naturally undergoes aging and wear, especially when exposed to the high heat of an engine bay. The chemical stability of the elastomer determines how well the belt resists cracking and stretching under constant tension.
Another critical component is the synchronization of the belt with its supporting accessories. A timing belt does not work in isolation; it relies on the timing belt tensioner and the water pump to maintain the correct alignment and pressure. If the tensioner fails, the wholesale conveyor belt may jump teeth, leading to an immediate loss of engine timing and severe mechanical damage.
Finally, the environmental conditions and the total mileage of the vehicle are the ultimate determinants of a belt's lifespan. Most manufacturers recommend a replacement cycle between 60,000 to 100,000 kilometers, with 80,000 km being the industry gold standard for preventative maintenance. Ignoring these cycles increases the risk of a sudden break, which is far more costly than a scheduled replacement.
Practical Applications and Industry Use Cases
The application of precision rubber belts extends far beyond the passenger car. In industrial zones, the use of a wholesale conveyor belt is essential for the automated transport of raw materials, where timing and grip are required to move goods across varying inclines without slippage. This is particularly evident in mining and logistics hubs where high-torque transmission is a daily requirement.
In specialized sectors, such as pharmaceutical manufacturing, these belts are engineered from non-contaminating materials to ensure that the movement of medicine remains sterile and precise. Similarly, in remote industrial zones, the ability to store bulk quantities of replacement belts prevents long-term shutdowns that could occur if a single critical component failed in a location far from a parts distributor.
Performance Comparison of Rubber Belt Procurement Methods
Long-Term Value of Preventative Replacement
The logical and emotional value of a preventative replacement strategy cannot be overstated. From a financial perspective, the cost of replacing a timing belt and its associated tensioners is a fraction of the cost of rebuilding an entire engine after a belt snap. By leveraging wholesale conveyor belt pricing, fleet operators can implement these schedules across hundreds of vehicles without straining their maintenance budgets.
Beyond the costs, there is the element of trust and safety. A vehicle that suffers a timing belt failure on a highway is not just a mechanical problem; it is a safety hazard. Ensuring that every belt is replaced at the 80,000 km mark provides peace of mind for the driver and reliability for the operator, fostering a culture of safety and innovation in fleet management.
Future Trends in Rubber Material Innovation
The future of the wholesale conveyor belt industry is moving toward "smart materials" and enhanced sustainability. New synthetic polymers are being developed that offer higher heat resistance and lower friction coefficients, which directly translates to better fuel efficiency and longer service intervals for automotive engines.
Digital transformation is also playing a role, with some high-end industrial belts incorporating embedded sensors to monitor wear and tear in real-time. Instead of relying on a fixed 80,000 km estimate, operators will soon be able to replace belts based on actual material degradation data, moving from preventative to predictive maintenance.
Furthermore, there is a significant push toward green chemistry. The shift away from harmful phthalates and the introduction of recyclable rubber composites ensure that the industrial expansion of the rubber parts industry does not come at the cost of the environment.
Overcoming Common Maintenance Challenges
One of the most common challenges in maintaining rubber belts is the failure to replace the entire "kit." Many operators make the mistake of replacing only the belt while leaving the old tensioner or water pump in place. This is a critical error, as an old, worn tensioner can put uneven pressure on a new wholesale conveyor belt, causing it to fail prematurely.
Another challenge is the inaccuracy of maintenance logs. In large-scale operations, tracking the exact mileage of every vehicle can be difficult. The solution lies in the implementation of automated fleet management software that triggers alerts when a vehicle approaches the 80,000 km threshold, ensuring no belt is left to a chance of breaking.
Finally, the market is often flooded with low-quality imitations. The only way to overcome this is by establishing long-term partnerships with verified manufacturers who adhere to ISO standards, ensuring that the rubber compound and tooth geometry are exactly as specified in the vehicle maintenance manual.
Comparison Analysis of Belt Maintenance and Sourcing Strategies
| Maintenance Strategy |
Risk Level |
Cost Efficiency |
Recommended Interval |
| Preventative Kit Replace |
Very Low |
High |
80,000 km |
| Belt Only Replacement |
Medium |
Medium |
60,000 km |
| Run-to-Failure |
Extreme |
Very Low |
N/A |
| Predictive Sensor Monitoring |
Low |
High (Long Term) |
Data-Driven |
| Retail Piece Sourcing |
Medium |
Low |
Manual Check |
| Wholesale Strategic Stock |
Low |
Very High |
Scheduled Batch |
FAQS
Rubber is a perishable material that degrades due to heat, friction, and time. By the 80,000 km mark, most belts have undergone significant structural fatigue. Replacing them proactively prevents a sudden snap, which would cause the pistons to hit the valves, resulting in catastrophic engine failure and expensive repairs.
The tensioner is responsible for keeping the belt tight. If an old tensioner is used with a new belt, it may provide uneven tension or vibrate, leading to premature wear on the new belt's teeth. This significantly increases the risk of the belt skipping a tooth, which throws off the engine timing.
No. While both are rubber products, automotive timing belts have specific tooth profiles and material compounds designed for high-speed synchronization and heat resistance. You must ensure that the belt matches the exact specifications in your vehicle's maintenance manual to ensure safety and functionality.
Unfortunately, timing belts often show few outward signs of failure until it is too late. Some may develop visible cracks or "glazing" (a shiny appearance), but the most reliable indicator is the odometer. Once you reach the manufacturer's recommended limit (typically 80,000 km), the belt should be replaced regardless of its appearance.
Metal chains offer greater stability and often last the life of the engine. However, they are noisier, heavier, and more expensive to install. Rubber belts are quieter and more efficient for many engine types, provided they are replaced on a strict schedule.
The best approach is to partner with a specialized manufacturer through wholesale channels. This ensures consistent quality, adherence to ISO standards, and significant cost savings compared to retail purchasing, allowing for a standardized maintenance schedule across all vehicles.
Conclusion
In summary, the precision and reliability of rubber timing and transport systems are the backbone of both automotive performance and industrial efficiency. By understanding the critical role of the belt as a "bridge" for force transfer and adhering to a strict preventative replacement cycle—ideally every 80,000 km—operators can avoid the devastating costs of mechanical failure. The shift toward high-quality wholesale conveyor belt sourcing allows for a sustainable balance between operational cost and system safety.
Looking ahead, the integration of smart materials and predictive maintenance will further redefine how we manage rubber components. We encourage fleet managers and industrial engineers to move beyond reactive repairs and embrace a strategic, bulk-sourcing approach to ensure long-term reliability and peace of mind. For premium quality rubber solutions and wholesale inquiries, visit our website: www.hawkbelt.com.